EN


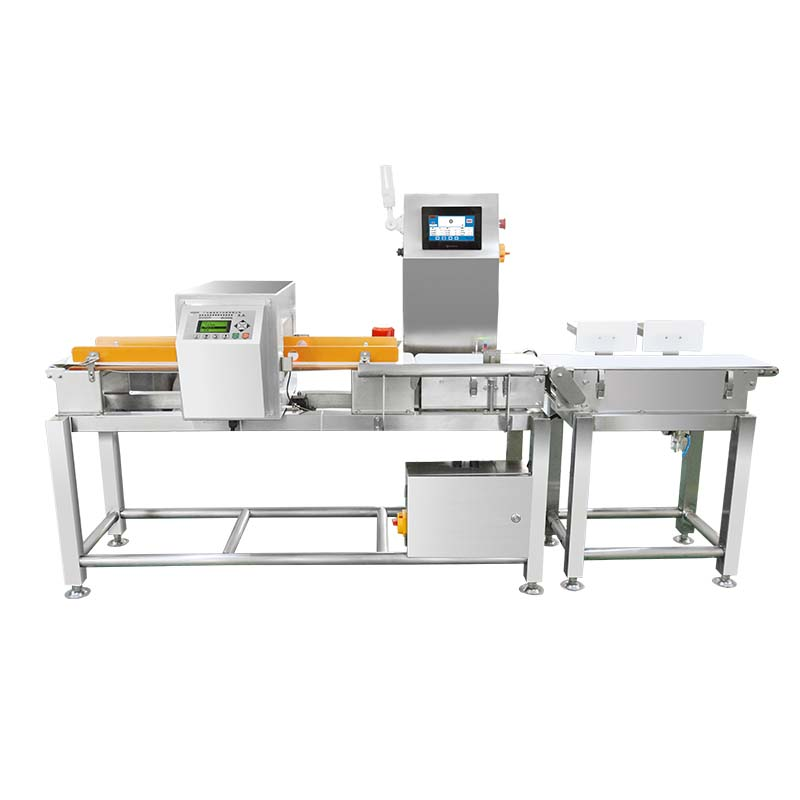
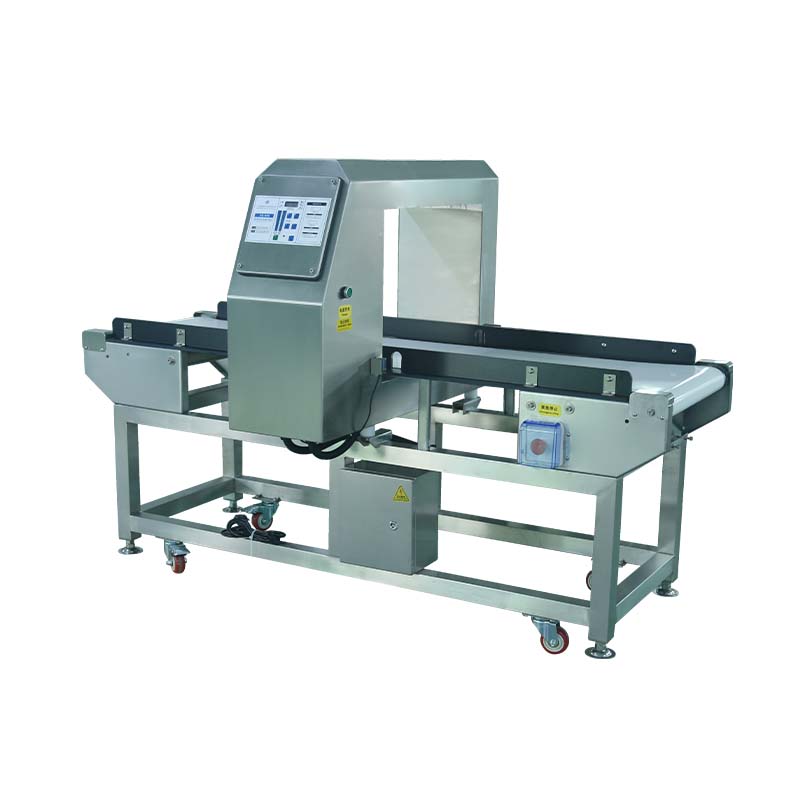
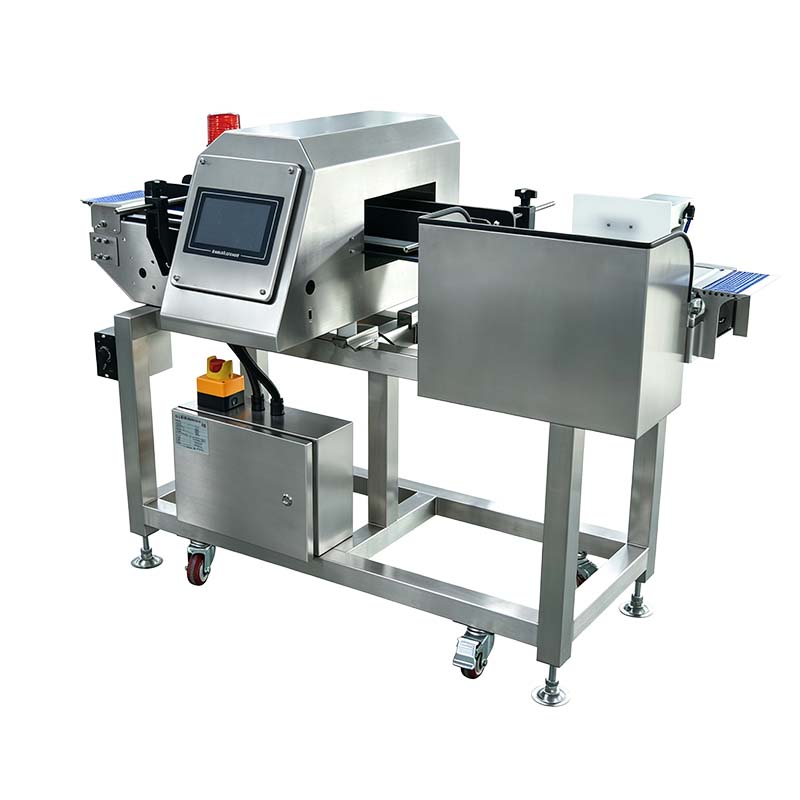
In the food processing industry, ensuring the safety and quality of products is paramount. This is especially true for products that are packaged and sold directly to consumers. An integrated check weight and metal detector system plays a crucial role in achieving this goal.
Scenario:
A leading producer of canned goods was facing challenges in maintaining the desired weight of its products while also ensuring the absence of metal contaminants. To address these issues, the company decided to invest in an integrated check weight and metal detector system.
System Description:
The system consists of a check weigher that verifies the weight of each can as it passes along the conveyor belt. Simultaneously, a metal detector scans the can for any traces of metal contamination.
Implementation:
The check weight and metal detector system was installed at the end of the filling line, immediately before the cans were sealed and labeled. The system was calibrated to detect even the smallest variations in weight and the tiniest metal fragments.
Benefits:
Conclusion:
The implementation of the integrated check weight and metal detector system has been a significant success for the canned goods producer. Not only has it improved the quality and safety of its products, but it has also enhanced the overall efficiency of the production process. This has enabled the company to maintain its competitive edge in the market while providing a safe and satisfying product to its customers.
 ONLINE