Conveyor Checkweigher | Precision Weight Control

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

conveyor checkweigher

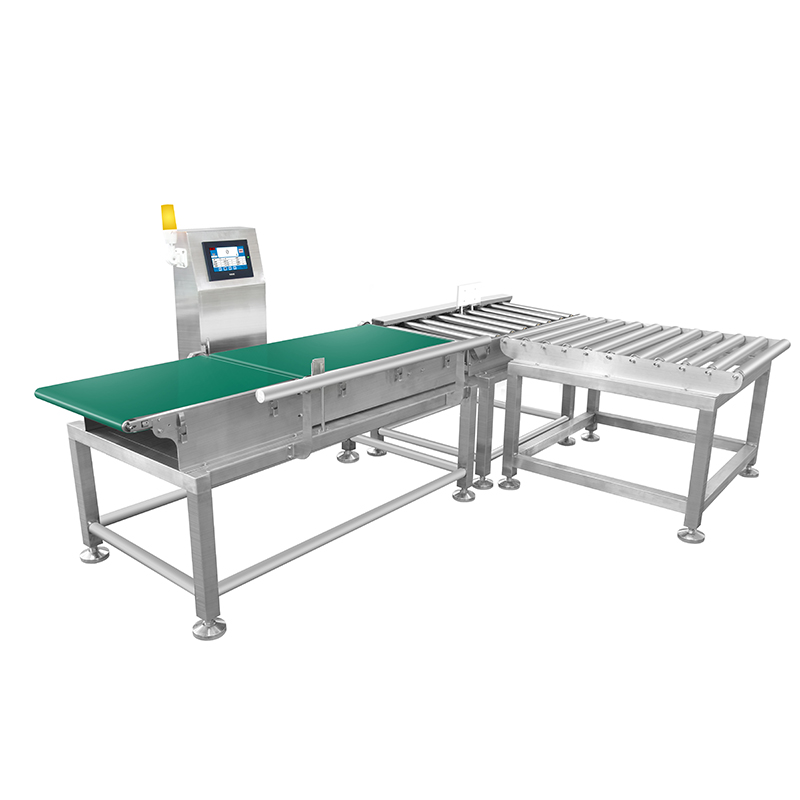
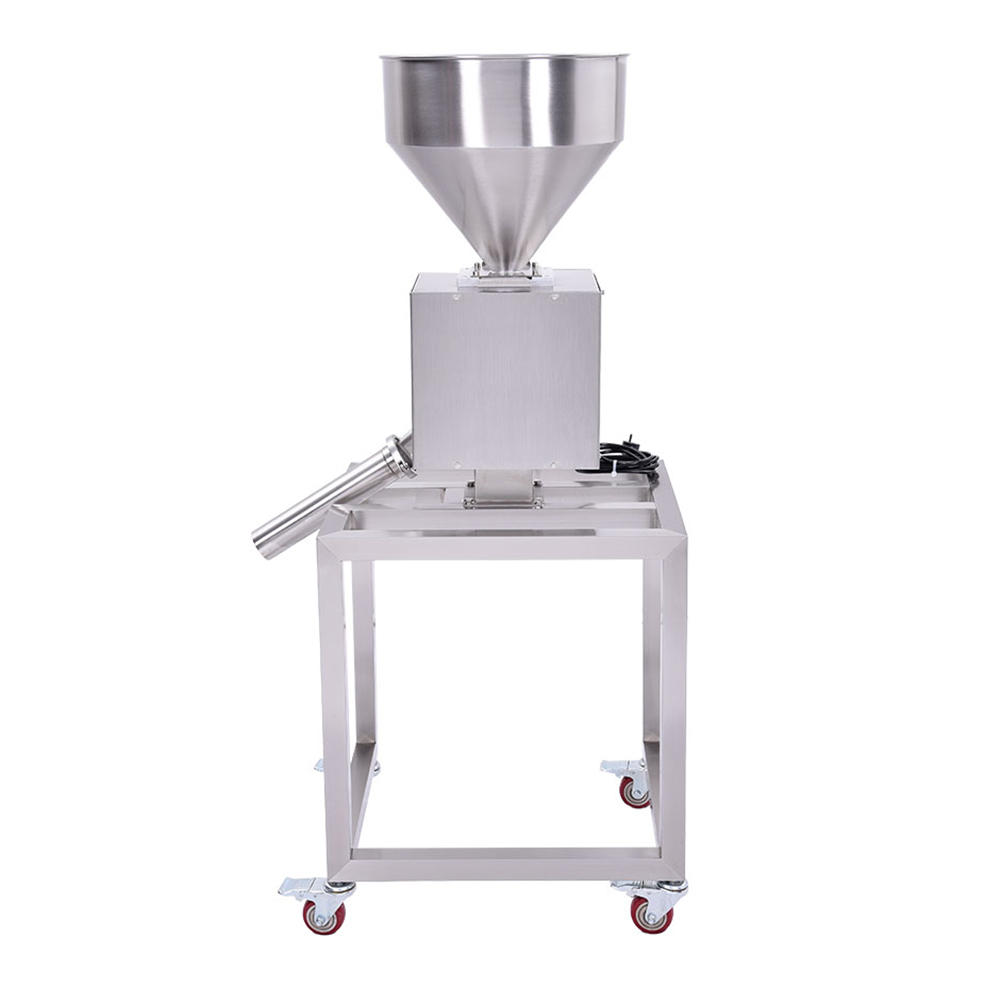
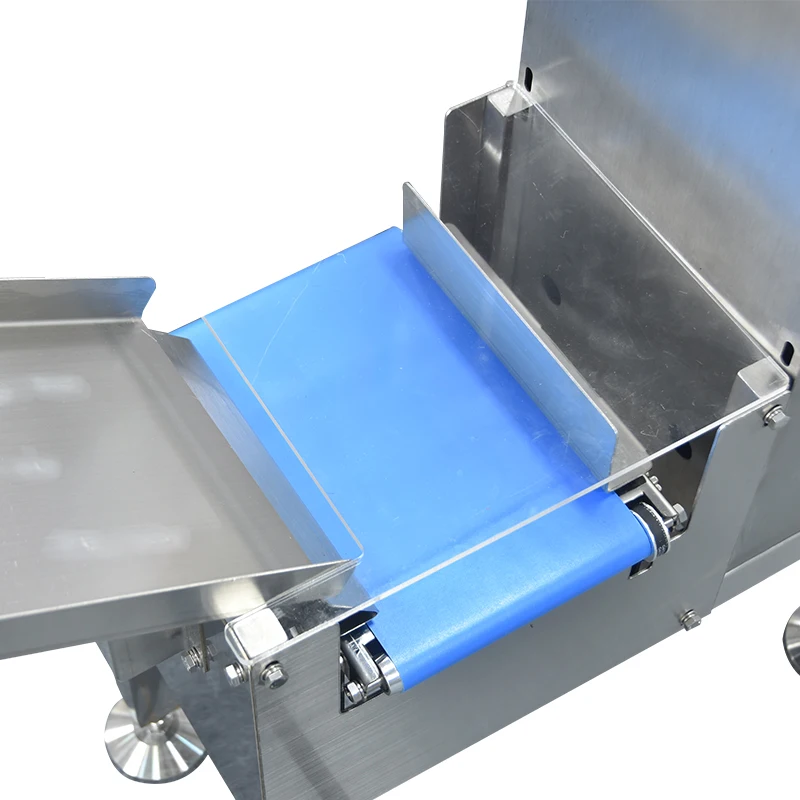
A conveyor checkweigher is an automated weighing system designed to monitor and verify the weight of products as they move along a production line. This sophisticated equipment serves as a critical quality control tool in manufacturing and packaging operations across multiple industries. The conveyor checkweigher operates by precisely measuring each item that passes through its sensors, ensuring that products meet specified weight requirements before they leave the facility. The primary function of a conveyor checkweigher is to detect underweight and overweight products automatically, maintaining consistency in product quality and regulatory compliance. Modern conveyor checkweigher technology integrates advanced load cells and digital processing systems that deliver real-time weight measurements with exceptional accuracy. These systems can process hundreds of items per minute, making them ideal for high-speed production environments. Key technological features of a conveyor checkweigher include adjustable weight thresholds, statistical data tracking, and automated rejection mechanisms. The conveyor checkweigher can interface with existing production systems through network connectivity, enabling seamless data integration and process optimization. Applications for conveyor checkweigher systems span food and beverage production, pharmaceuticals, cosmetics, and consumer goods manufacturing. Whether you require dynamic weighing for packaged foods, pharmaceuticals, or industrial products, a conveyor checkweigher delivers reliable performance and measurable results for your operation.

Popular Products

A conveyor checkweigher offers substantial operational benefits that directly improve your bottom line and product quality. The primary advantage is cost reduction through waste elimination. By automatically detecting underweight products before shipment, a conveyor checkweigher prevents costly give-aways and protects your profit margins. Simultaneously, it identifies overweight items, reducing material costs and improving efficiency across your production process. Regulatory compliance represents another critical benefit. A conveyor checkweigher generates comprehensive documentation and audit trails that satisfy food safety, pharmaceutical, and consumer protection regulations. This documentation protects your company from fines and recalls, providing peace of mind and operational security. Your customers receive consistently accurate products, strengthening brand reputation and customer loyalty. Operational efficiency improves dramatically with a conveyor checkweigher integrated into your line. Real-time monitoring enables immediate corrective action when weight variations occur, minimizing production disruptions. The conveyor checkweigher reduces manual inspection requirements, freeing staff for higher-value tasks while improving accuracy beyond human capabilities. Statistical data collection helps identify systemic issues before they become major problems. The conveyor checkweigher adapts to various product types and packaging formats with minimal setup time. Whether handling fragile items, bulk products, or specialty packaging, this versatile system maintains consistent performance. Integration capabilities allow your conveyor checkweigher to communicate with manufacturing execution systems, creating a cohesive production environment. Investment in a conveyor checkweigher delivers rapid return on investment through improved efficiency, reduced waste, and enhanced quality control throughout your operation.

Practical Tips

Advanced Check Weigher Technology Revolutionizes Production Line Efficiency

21

Aug

Advanced Check Weigher Technology Revolutionizes Production Line Efficiency

Achieve optimal sorting accuracy with our industrial weight sorters, including automatic and precision weight sorting equipment. Ideal for industries requiring high precision in weight-based sorting.
View More
Integrated Check Weight & Metal Detector Boosts Manufacturing Efficiency

21

Aug

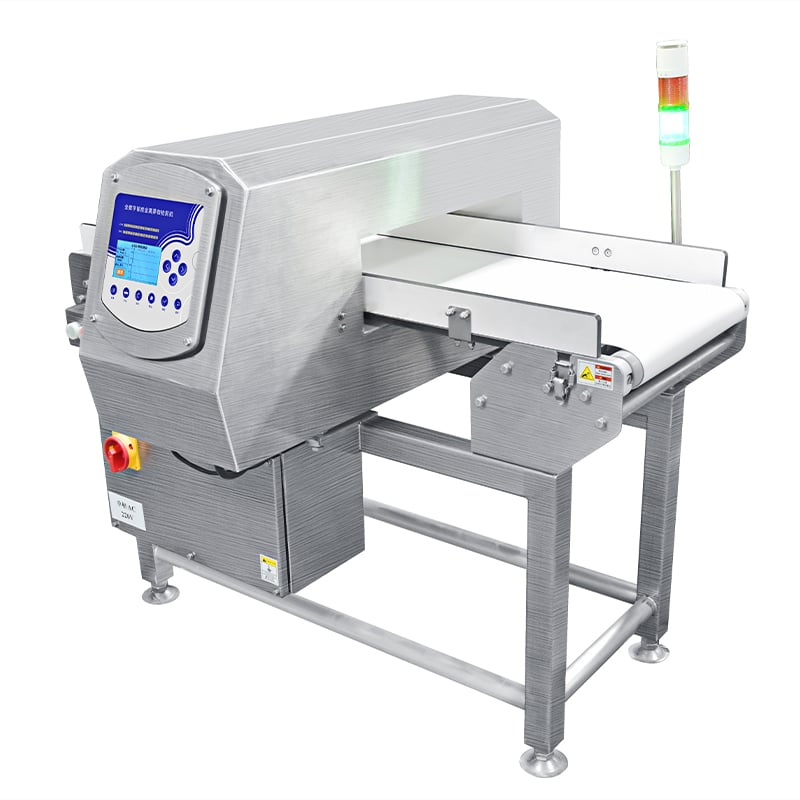
Integrated Check Weight & Metal Detector Boosts Manufacturing Efficiency

Ensure food safety with our reliable food metal detectors, including the best and hot-selling models. These low-cost detectors are perfect for maintaining high safety standards in food processing.
View More
Reigning Productivity with Ywan Test Logistics Sorting Machinery

28

Apr

Reigning Productivity with Ywan Test Logistics Sorting Machinery

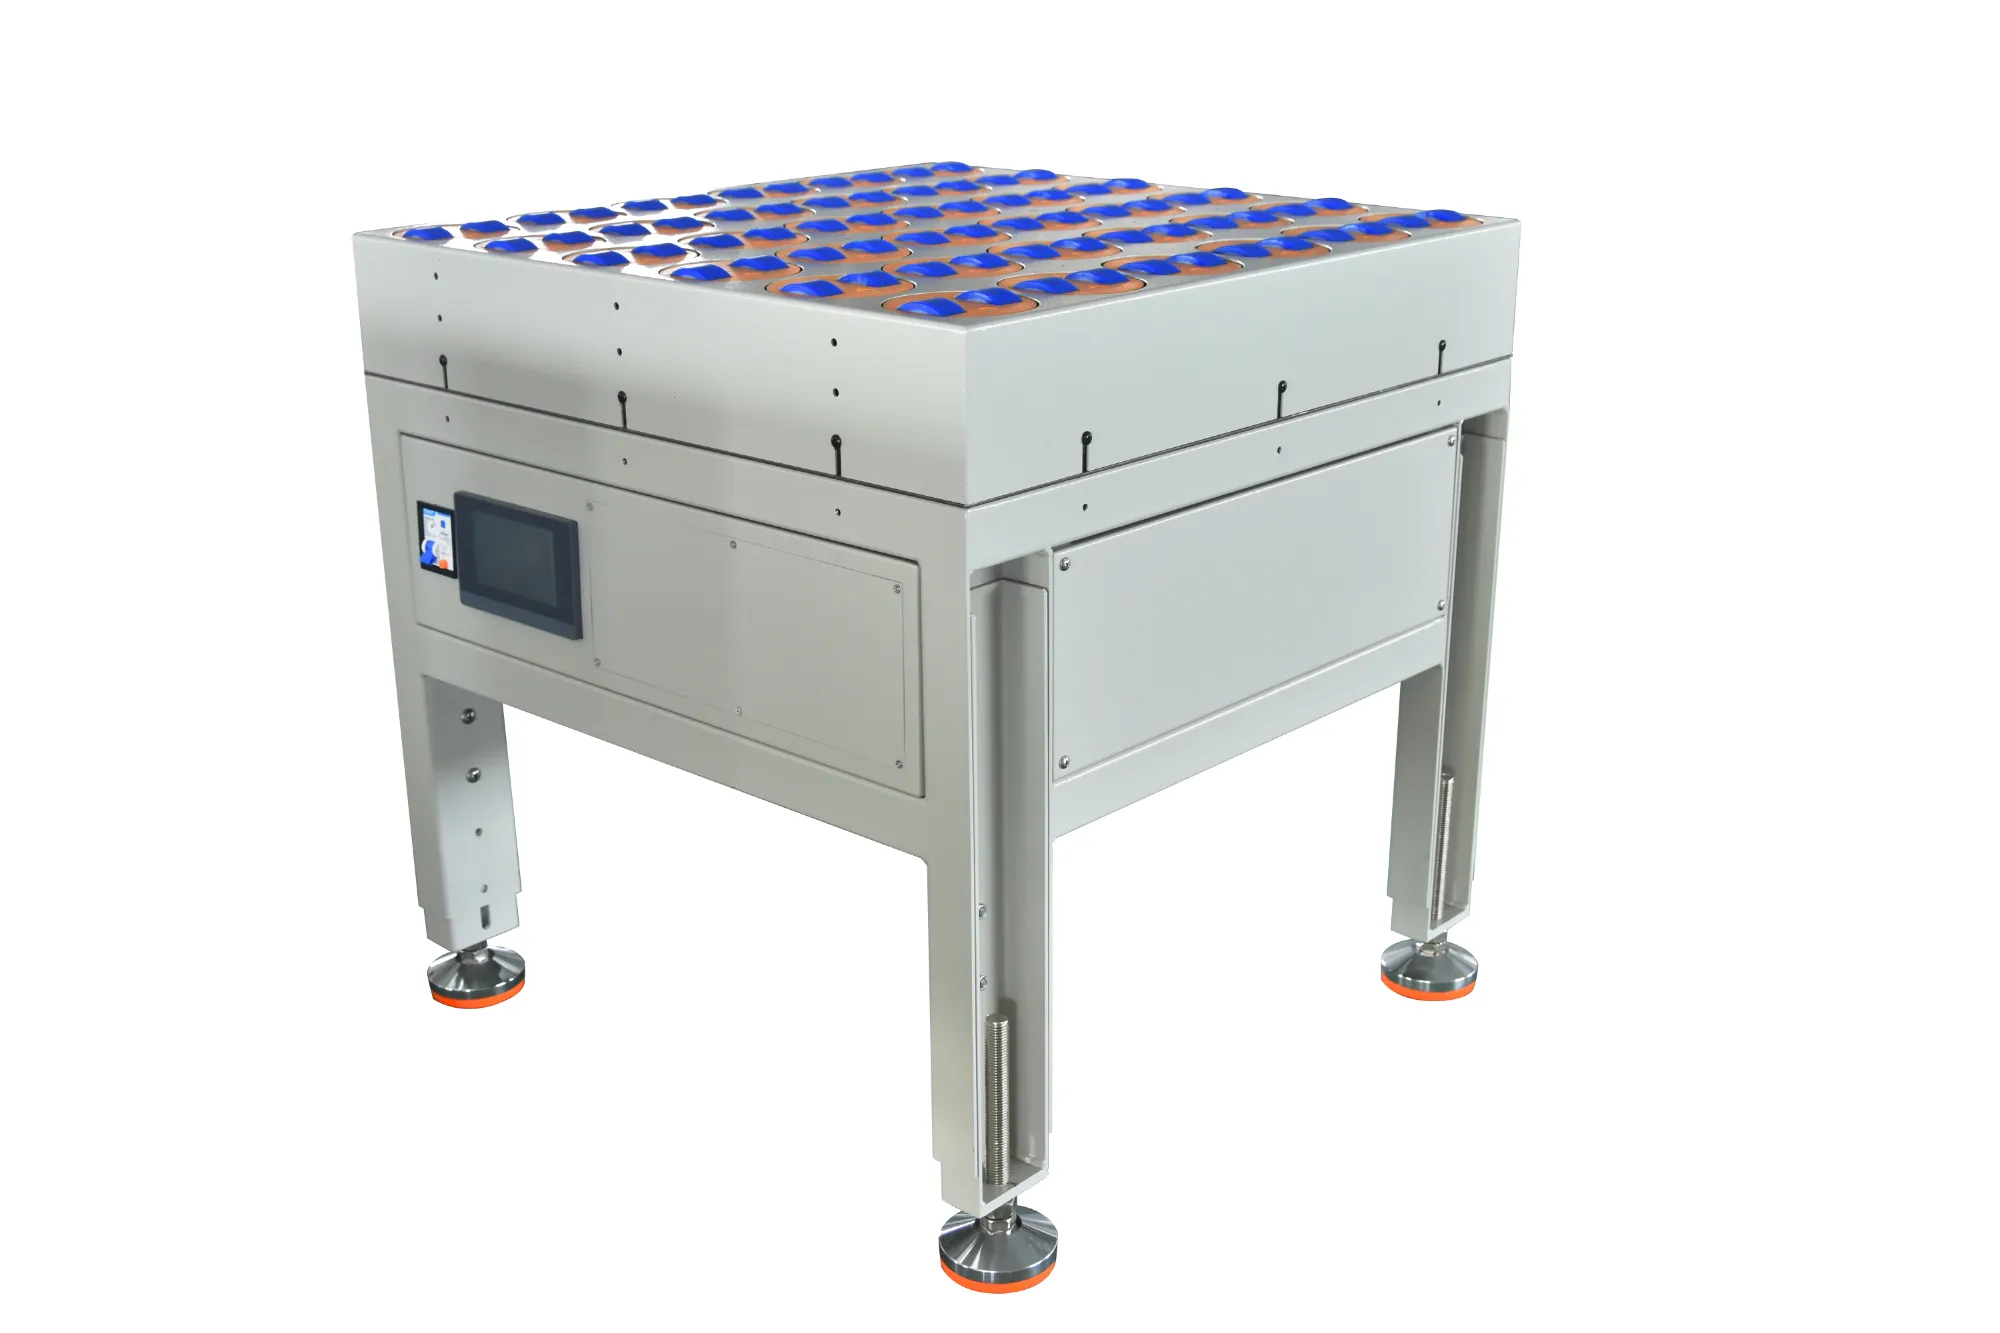
Ywan Test revolutionizes logistics with high-speed, precise sorting machinery, boosting efficiency, reducing costs, and enhancing customer satisfaction.
View More
Ywan Test Automated Package Sorter Systems In The Logistics Sector

09

Sep

Ywan Test Automated Package Sorter Systems In The Logistics Sector

Ywan Test's automated package sorters boost logistics efficiency with high-speed, accurate sorting, reducing costs and enhancing customer satisfaction.
View More

conveyor checkweigher

Advanced Measurement Precision and Speed

Advanced Measurement Precision and Speed

The conveyor checkweigher delivers exceptional measurement accuracy while maintaining impressive throughput speeds. Modern conveyor checkweigher systems utilize sophisticated load cell technology that can detect weight variations as small as a fraction of a gram, ensuring product consistency at unprecedented levels. This precision is maintained even at production speeds exceeding 500 items per minute, a capability that distinguishes premium conveyor checkweigher systems from standard alternatives. The technical architecture of a conveyor checkweigher incorporates dynamic weighing algorithms that account for product motion, eliminating inaccuracies associated with traditional static weighing methods. This means your conveyor checkweigher provides reliable measurements regardless of conveyor speed variations or product acceleration patterns. For manufacturers requiring both accuracy and speed, a conveyor checkweigher represents the optimal solution. The system's ability to deliver consistent results across high-volume production runs makes it invaluable for competitive manufacturing environments where quality and efficiency directly impact profitability and market position.
Intelligent Rejection and Process Control

Intelligent Rejection and Process Control

Your conveyor checkweigher incorporates intelligent rejection capabilities that automatically remove out-of-specification products from your production line in real-time. This automated rejection mechanism prevents defective items from reaching customers, protecting your brand reputation and eliminating costly recalls. The conveyor checkweigher's rejection system can be customized to handle various product types, from delicate items requiring gentle removal to heavy industrial products needing forceful diversion. The conveyor checkweigher integrates seamlessly with statistical process control systems, enabling predictive quality management. When your conveyor checkweigher detects trending weight variations, operators receive alerts that facilitate preventive maintenance or process adjustments before rejections increase. This proactive approach maximizes production efficiency and minimizes waste. The conveyor checkweigher's reporting capabilities provide actionable insights into production performance, helping managers identify optimization opportunities. By combining immediate rejection with advanced analytics, your conveyor checkweigher system transforms quality control from reactive problem-solving into strategic process improvement.
Flexibility and Integration with Modern Manufacturing

Flexibility and Integration with Modern Manufacturing

A conveyor checkweigher adapts to diverse production environments and seamlessly integrates with your existing manufacturing infrastructure. Whether your facility uses legacy systems or cutting-edge Industry 4.0 technology, a conveyor checkweigher can be configured to communicate effectively with your equipment ecosystem. This flexibility eliminates costly facility overhauls and accelerates implementation timelines significantly. The conveyor checkweigher supports multiple connectivity options including Ethernet, serial communication, and wireless protocols, ensuring compatibility with various production management systems. Custom integration capabilities mean your conveyor checkweigher can trigger automated responses in downstream processes, creating an optimized manufacturing workflow. Whether you produce food products, pharmaceuticals, or consumer goods, a conveyor checkweigher accommodates different product dimensions, weights, and packaging configurations with minimal reconfiguration. This adaptability makes a conveyor checkweigher an investment-protected solution that grows with your business needs and evolving technology landscape.

Related Search

Conveyor Checkweigher | Precision Weight Control