Conveyor Weight Checker | Precision Quality Control

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

conveyor weight checker

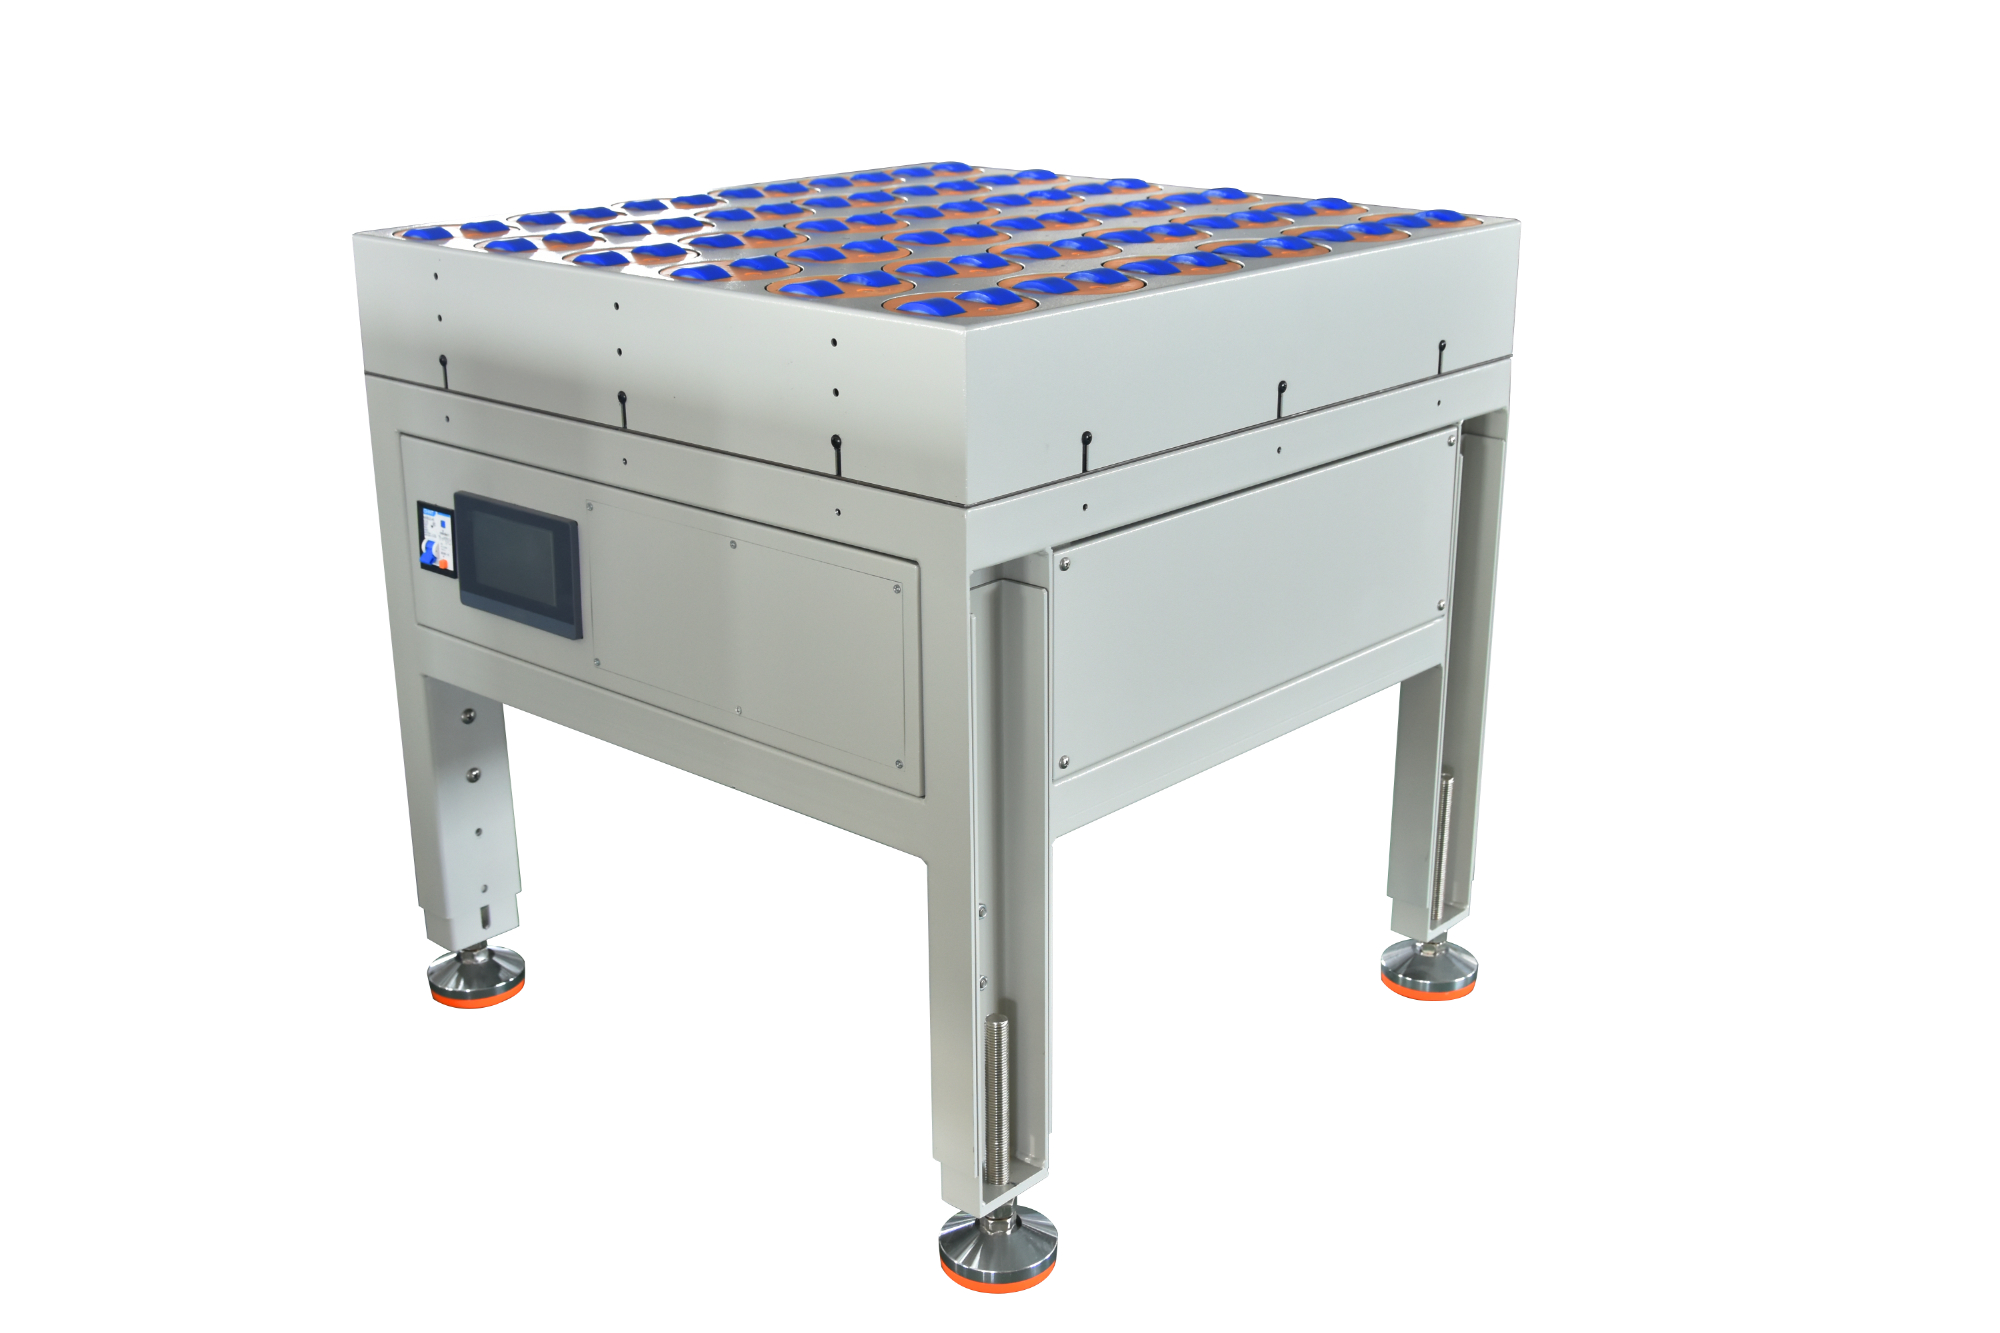
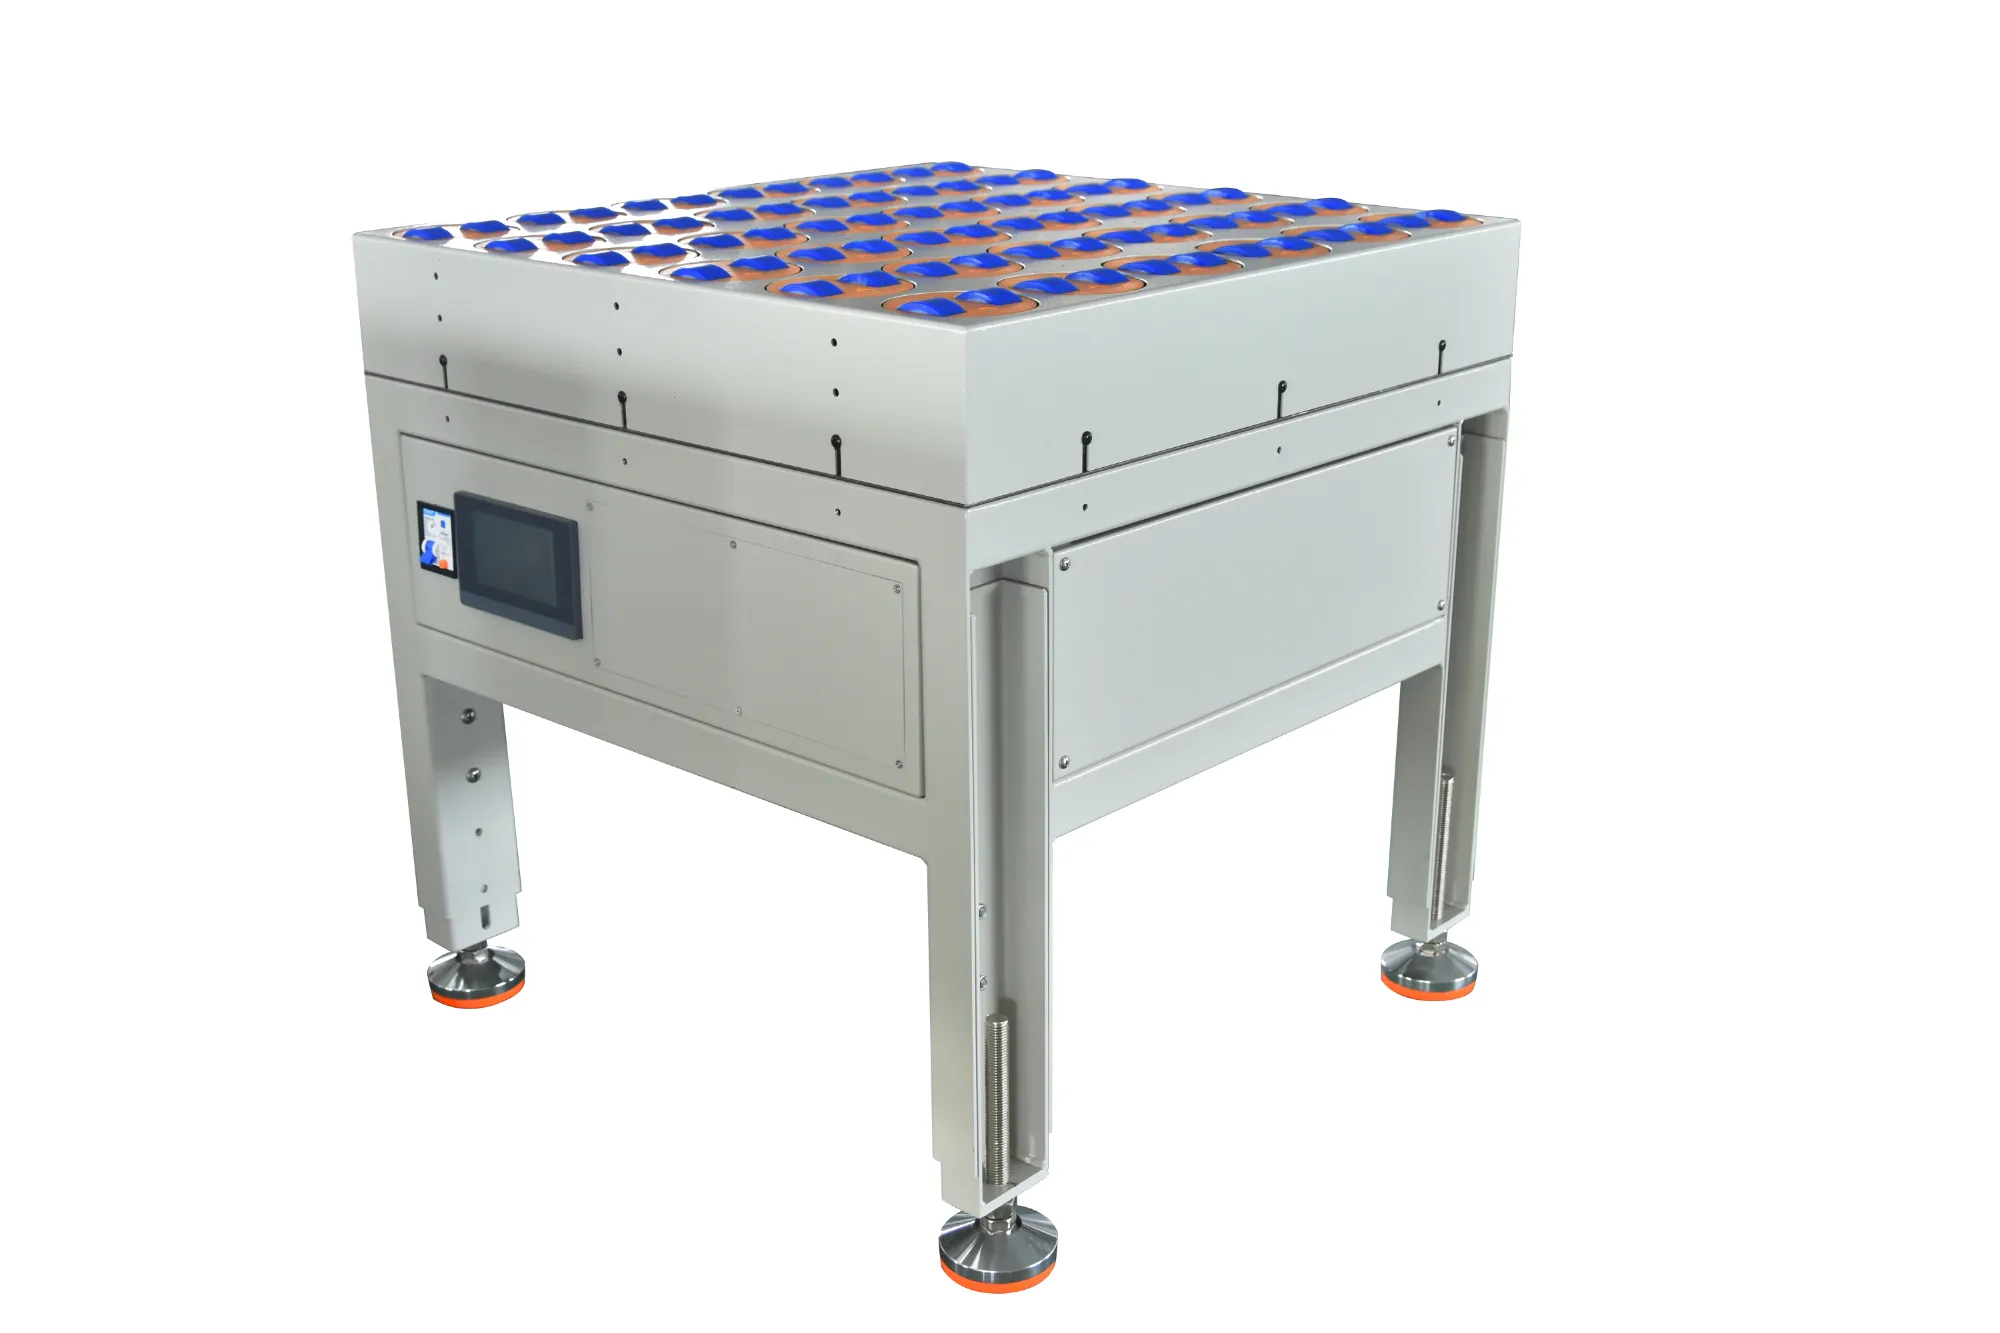
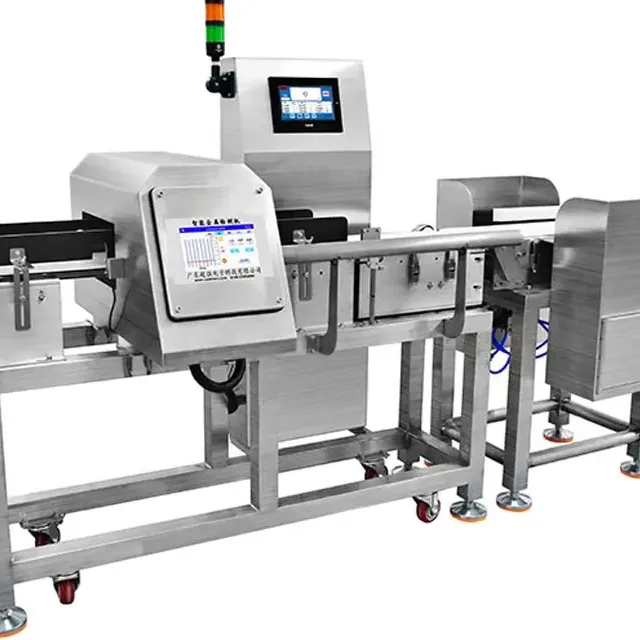
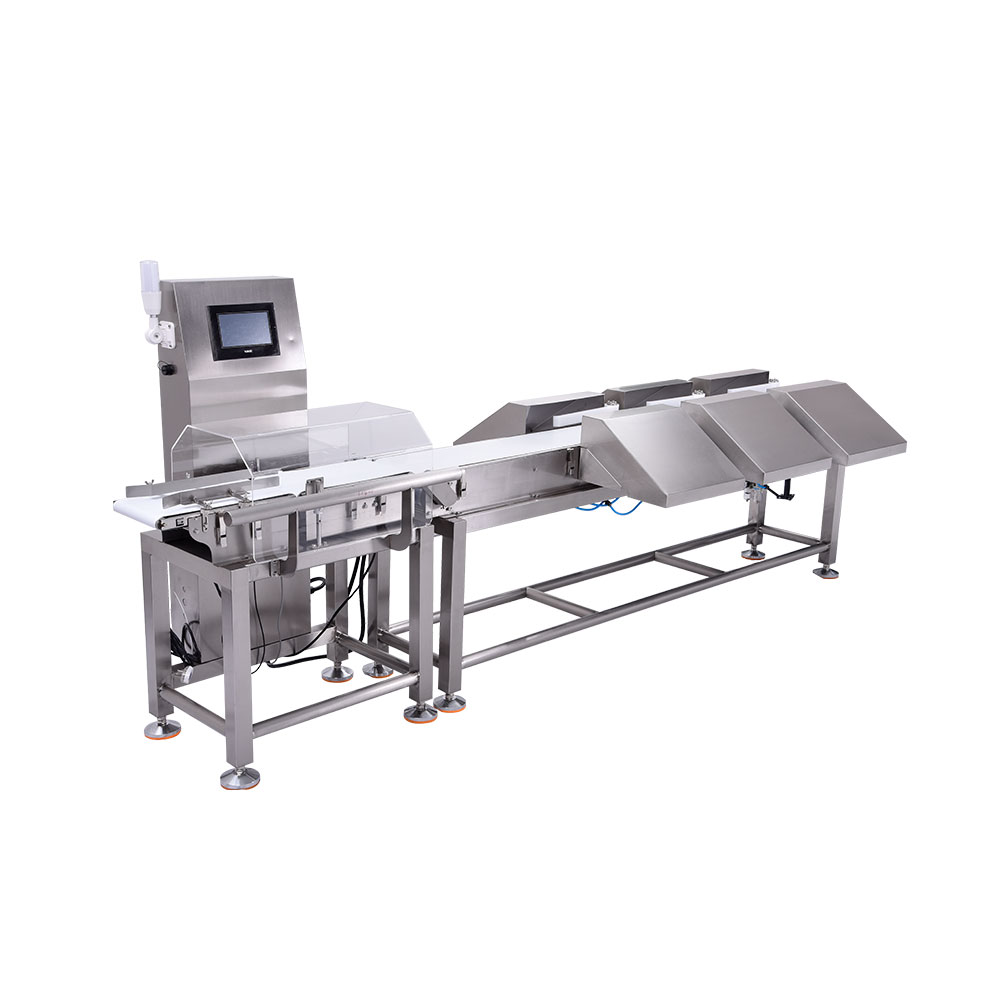
A conveyor weight checker is an essential industrial device designed to measure and monitor the weight of products moving along conveyor belt systems in real-time. This advanced conveyor weight checker integrates precision sensors and digital processing technology to ensure accurate mass detection throughout production operations. The primary function of a conveyor weight checker involves capturing weight data from items passing across the belt, transmitting this information to central monitoring systems, and triggering alerts when products fall outside predetermined weight specifications. Modern conveyor weight checker systems utilize load cell technology and sophisticated signal processing algorithms to deliver exceptional accuracy regardless of conveyor speed variations. These devices operate seamlessly with existing production infrastructure, requiring minimal setup modifications. The conveyor weight checker accommodates various product sizes, shapes, and material compositions, making it versatile across multiple manufacturing sectors. Applications for a conveyor weight checker span numerous industries including food processing, pharmaceuticals, packaging, automotive components, and chemical manufacturing. In food production, the conveyor weight checker ensures portion control and regulatory compliance. Pharmaceutical manufacturers rely on conveyor weight checker systems for precise dosage verification. Manufacturing facilities use conveyor weight checker technology to maintain quality standards and reduce material waste. The system's real-time data collection enables rapid rejection of non-compliant products, preventing defective items from reaching customers and protecting brand reputation. The conveyor weight checker represents a critical investment for facilities prioritizing production efficiency and quality assurance. Its technological sophistication combined with practical reliability makes it an indispensable component of modern industrial operations seeking consistent output excellence.

New Product Releases

A conveyor weight checker delivers substantial operational improvements that directly impact your production efficiency and profitability. The primary advantage lies in eliminating manual weight verification processes, which are time-consuming, error-prone, and labor-intensive. By implementing a conveyor weight checker, you automate quality control, allowing your team to focus on higher-value tasks while reducing labor costs significantly. The conveyor weight checker provides real-time weight monitoring that catches defects immediately during production, rather than discovering them during final quality inspections. This early detection prevents costly rework, material waste, and customer returns. You'll experience improved compliance with regulatory requirements, as the conveyor weight checker maintains detailed records of every product weight measurement, creating comprehensive audit trails essential for industry certifications. Operational benefits extend to increased production throughput. Unlike manual checking that slows conveyor speeds, a conveyor weight checker operates at full belt capacity without creating bottlenecks. The device integrates seamlessly with existing systems, including sorting mechanisms and rejection equipment, enabling automated responses to out-of-specification products. For businesses in food, pharmaceutical, or chemical industries, the conveyor weight checker ensures consistent product quality that strengthens customer confidence and brand loyalty. The system reduces material costs by identifying weight variations early, preventing expensive waste later in production. Installation of a conveyor weight checker typically yields return on investment within months through combined savings from waste reduction, labor efficiency, and improved customer satisfaction. The conveyor weight checker transforms your quality assurance from reactive to proactive, positioning your facility as a reliable producer while simultaneously enhancing your bottom line through measurable cost reductions and improved operational control.

Latest News

Reigning Productivity with Ywan Test Logistics Sorting Machinery

28

Apr

Reigning Productivity with Ywan Test Logistics Sorting Machinery

Ywan Test revolutionizes logistics with high-speed, precise sorting machinery, boosting efficiency, reducing costs, and enhancing customer satisfaction.
View More
Warehouse Automation Sorter Streamlining Operations for Enhanced Efficiency

08

Oct

Warehouse Automation Sorter Streamlining Operations for Enhanced Efficiency

Ywan Test's automation sorters enhance warehouse efficiency by speeding up operations, reducing labor costs, and improving accuracy.
View More
High-Speed Sorting Machines for Automated Logistics

23

Oct

High-Speed Sorting Machines for Automated Logistics

High-speed sorting machines by Ywan Test enhance logistics efficiency, boosting productivity and accuracy while reducing costs.
View More
Industrial Weight Sorter for Precision Sorting Applications

23

Oct

Industrial Weight Sorter for Precision Sorting Applications

Ywan Test's industrial weight sorter enhances precision and efficiency in manufacturing, ensuring quality control and streamlined production.
View More

conveyor weight checker

Precision Measurement Technology in Conveyor Weight Checker Systems

Precision Measurement Technology in Conveyor Weight Checker Systems

The conveyor weight checker incorporates advanced load cell sensors capable of detecting weight variations as small as 0.1 grams, ensuring exceptional measurement accuracy across all product types. This precision technology represents the cornerstone of effective quality control in modern manufacturing environments. The conveyor weight checker utilizes multi-point sensing arrays that capture weight data from different belt positions, eliminating blind spots and ensuring comprehensive coverage of every item passing through your production line. The sensor integration within a conveyor weight checker processes information thousands of times per second, providing instantaneous feedback about product specifications. This technological sophistication means your conveyor weight checker identifies defective items before they progress further down the production chain, preventing costly errors. The system's calibration stability ensures that a conveyor weight checker maintains accuracy even under challenging factory conditions including temperature fluctuations, vibration, and dust exposure. Regular maintenance protocols keep your conveyor weight checker performing at peak efficiency, delivering reliable measurements year after year for consistent quality assurance and operational excellence.
Real-Time Data Integration and Automated Responses

Real-Time Data Integration and Automated Responses

A conveyor weight checker revolutionizes quality control by providing instantaneous data transmission to your production management systems and central monitoring dashboards. This real-time capability means supervisors receive immediate alerts whenever a conveyor weight checker detects products outside acceptable weight ranges, enabling rapid corrective action before defects multiply. The conveyor weight checker connects seamlessly with automated rejection systems, sorting mechanisms, and production line controllers through industry-standard interfaces. The intelligence built into modern conveyor weight checker systems enables sophisticated analysis of weight distribution trends, helping operators identify potential equipment malfunctions before they compromise product quality significantly. Historical data collected by your conveyor weight checker creates valuable insights into production patterns, material consistency, and equipment performance over extended periods. This comprehensive record management makes a conveyor weight checker invaluable for regulatory audits, quality documentation, and continuous improvement initiatives. Integration capabilities ensure your conveyor weight checker communicates effectively with existing enterprise resource planning systems, material handling equipment, and quality management software, creating cohesive operations that maximize efficiency.
Cost Reduction and Return on Investment Benefits

Cost Reduction and Return on Investment Benefits

Installing a conveyor weight checker delivers measurable financial returns through multiple cost-reduction channels that improve your facility's bottom line substantially. The primary savings mechanism involves eliminating manual weight verification labor, reducing staffing requirements and associated payroll expenses significantly. A conveyor weight checker reduces material waste by identifying weight deviations early, preventing expensive rework and product scrapping that diminishes profitability. These combined savings typically generate positive return on investment within six to eighteen months depending on production volume and product specifications. The conveyor weight checker prevents costly customer returns and warranty claims by ensuring only compliant products reach markets, protecting your brand reputation and customer relationships. Reduced rejection rates downstream mean lower costs in final inspections, packaging, and shipping of defective items that your conveyor weight checker successfully identified earlier. Many facilities discover that a conveyor weight checker enables increased production speeds without sacrificing quality, effectively multiplying revenue generation from existing equipment. Energy efficiency improvements and extended equipment lifespan from reduced strain contribute additional long-term savings as your conveyor weight checker demonstrates its comprehensive value proposition to stakeholders and decision-makers.

Related Search

Conveyor Weight Checker | Precision Quality Control