Industrial Checkweigher - Precision Weight Control

Get a Free Quote

Our representative will contact you soon.
Email
Name
Company Name
Message
0/1000

industrial checkweigher

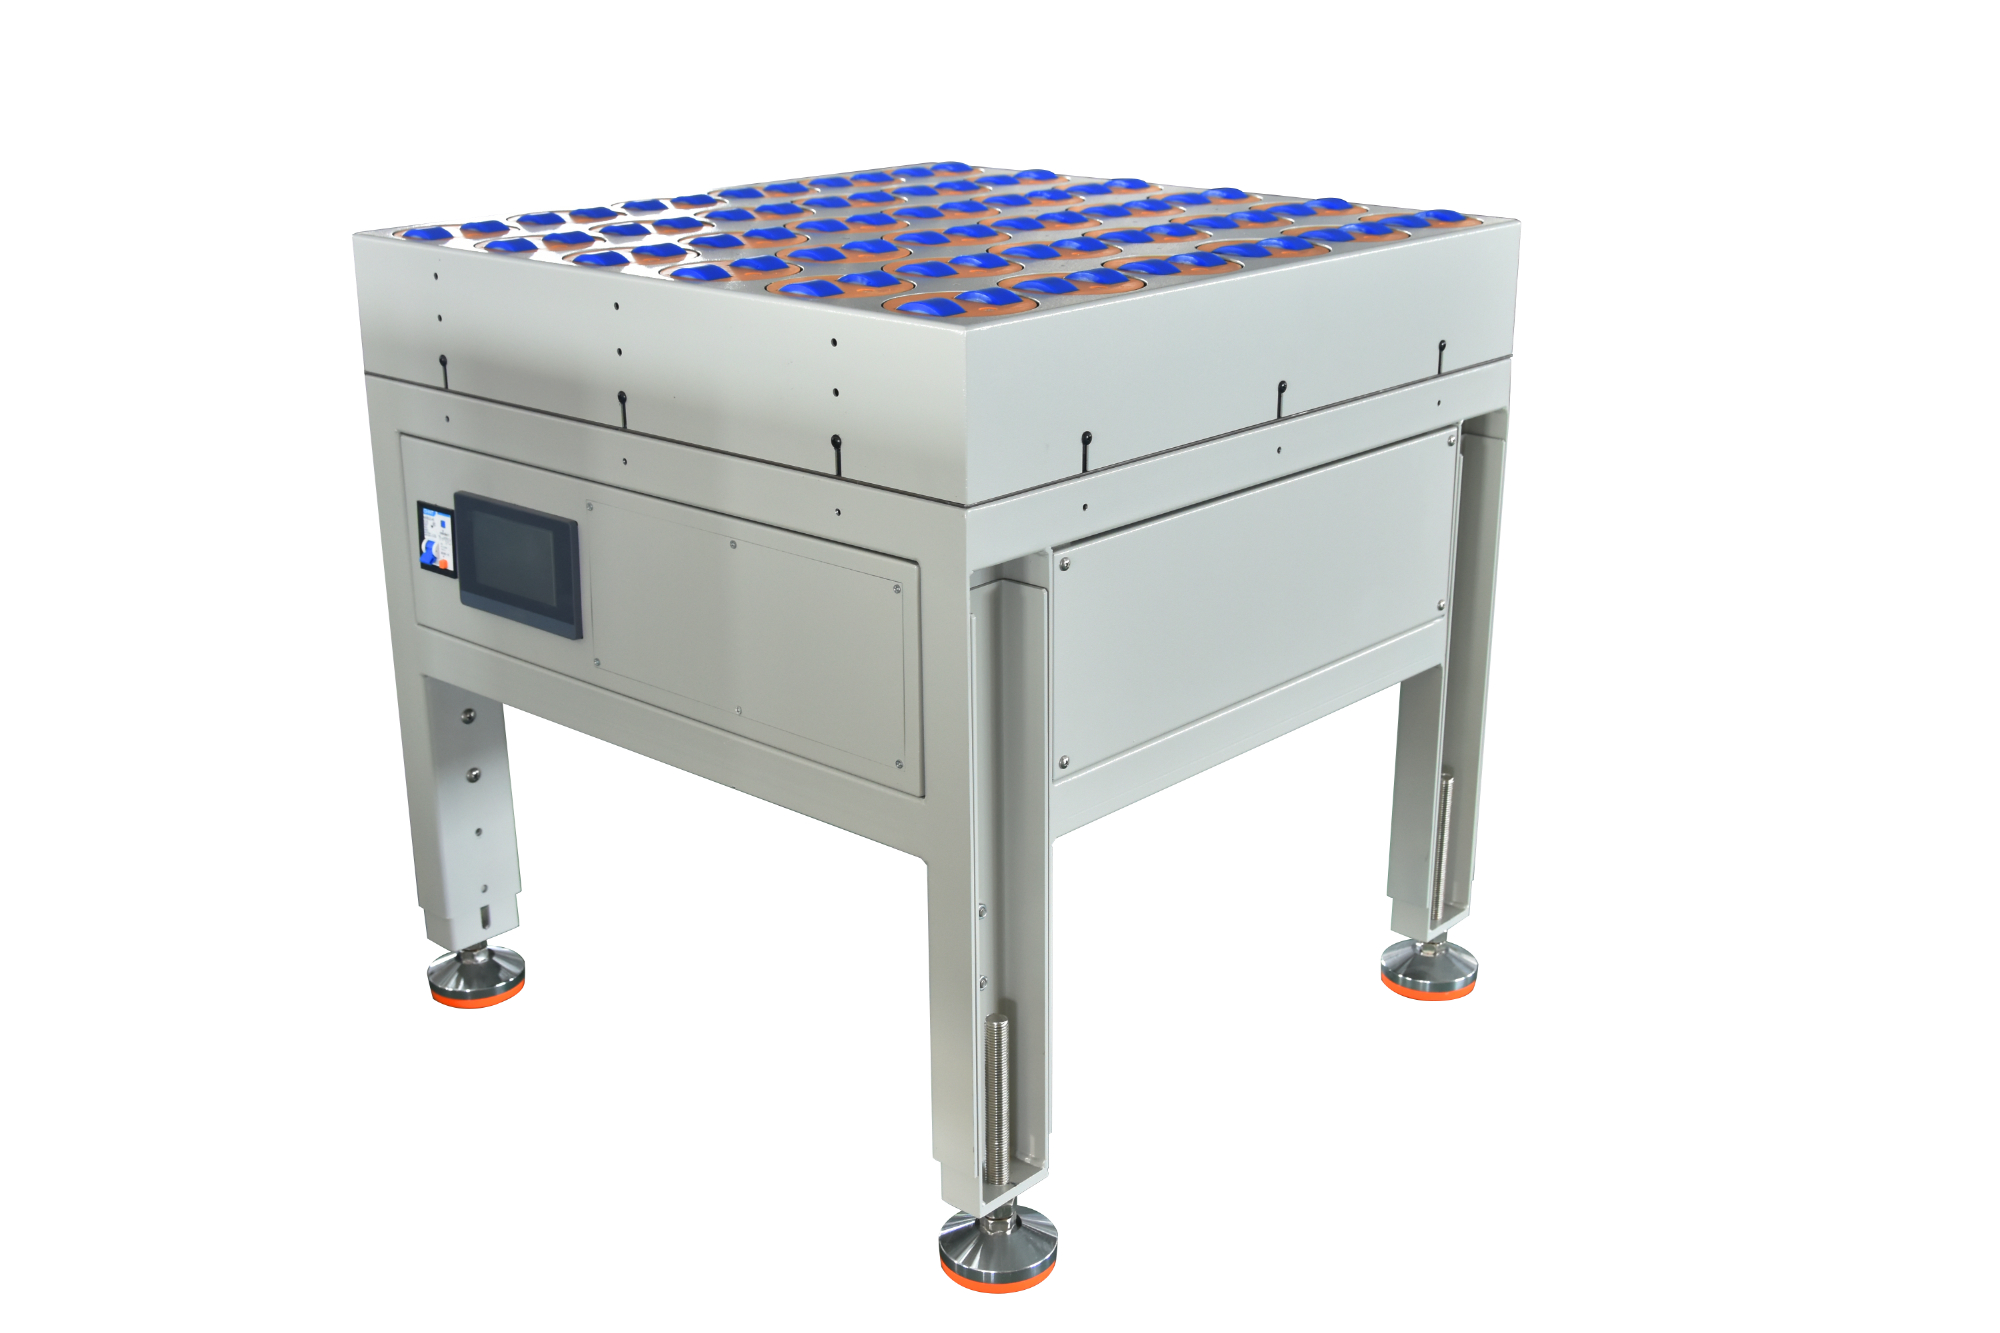
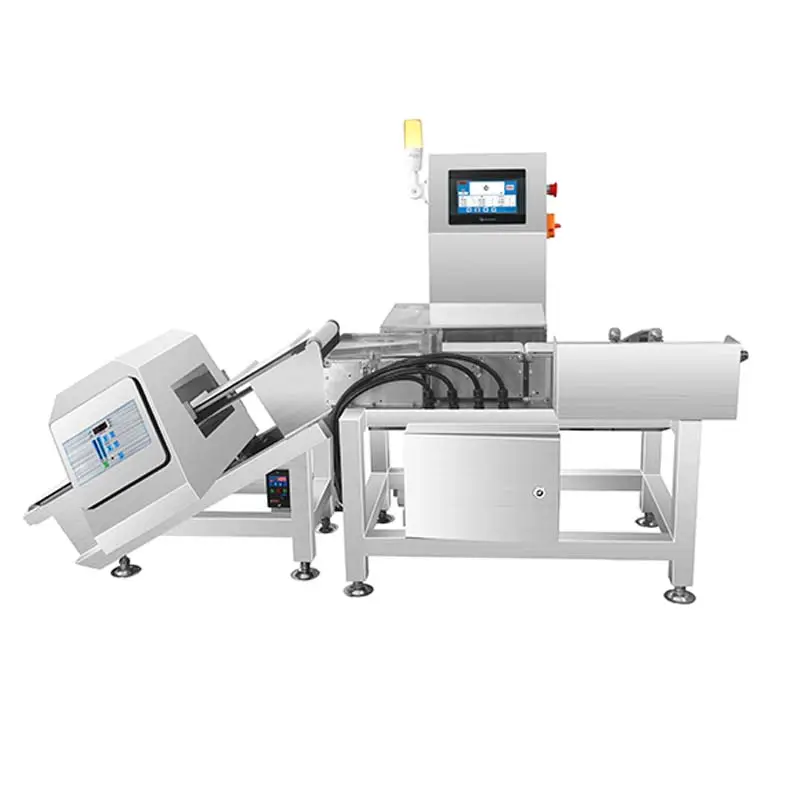
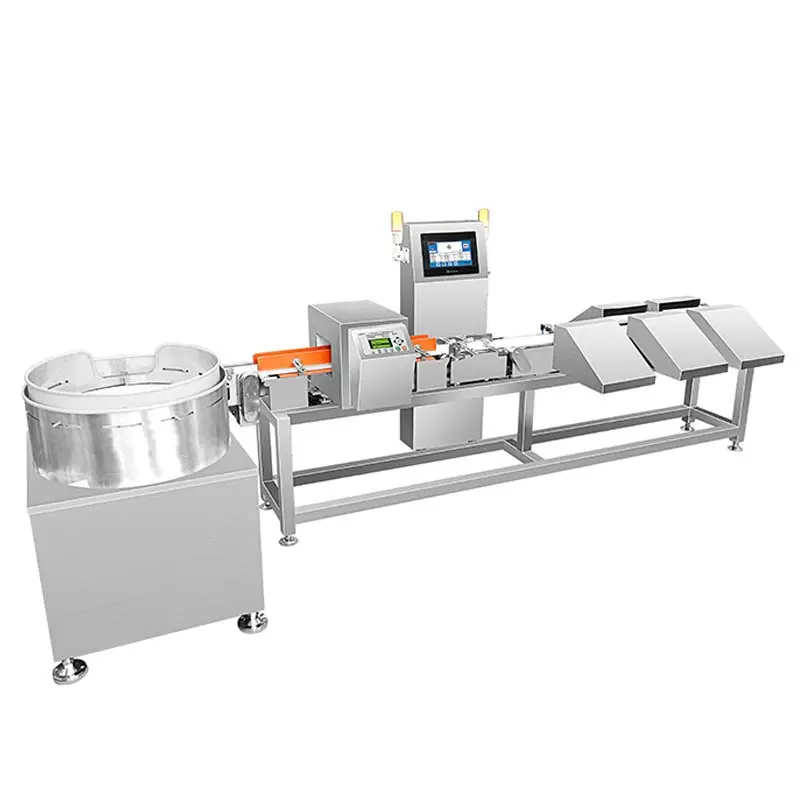
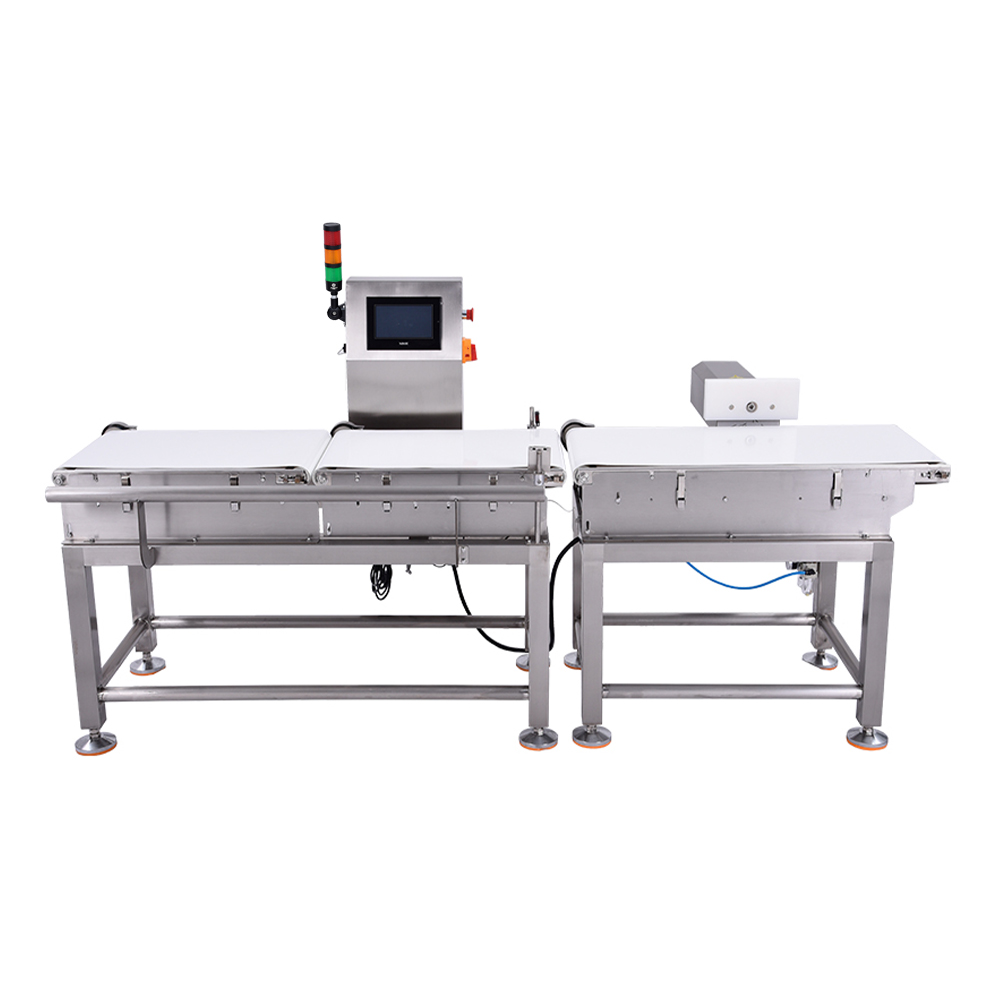
An industrial checkweigher is a precision weighing device designed to automatically measure and verify the weight of products during manufacturing and packaging operations. This sophisticated equipment ensures that every item meets exact weight specifications, making it an essential component in quality control processes across numerous industries. The industrial checkweigher operates by placing products on a conveyor belt or platform where sensors accurately detect weight variations in real-time. The core function of an industrial checkweigher involves detecting underweight and overweight items, which are then automatically rejected or diverted from the production line. Modern industrial checkweigher systems incorporate advanced technological features including high-speed processing capabilities, digital displays, and connectivity options for data logging. These devices utilize load cells and sophisticated algorithms to provide measurements accurate to fractions of a gram. An industrial checkweigher can process hundreds of items per minute, significantly improving production efficiency. The technology behind contemporary industrial checkweigher units includes stainless steel construction for hygiene, intuitive interfaces for easy operation, and customizable rejection systems. Applications for an industrial checkweigher span pharmaceutical packaging, food production, cosmetics manufacturing, and chemical processing. The industrial checkweigher addresses critical business needs by reducing waste, ensuring regulatory compliance, and protecting brand reputation. Industries relying on weight-sensitive products depend on industrial checkweigher technology to maintain consistent quality standards and customer satisfaction throughout their operations.

New Products

An industrial checkweigher delivers significant practical benefits that directly impact business profitability and operational excellence. By automatically detecting weight discrepancies, an industrial checkweigher eliminates the need for manual weight verification, reducing labor costs substantially while improving accuracy rates beyond human capability. The primary buyer value of an industrial checkweigher lies in waste reduction and cost savings, as it prevents underweight products from reaching customers and stops overweight items that compromise profit margins. Operational benefits include seamless integration into existing production lines, with most industrial checkweigher models offering plug-and-play installation that minimizes downtime. An industrial checkweigher provides real-time data tracking and reporting capabilities, enabling manufacturers to identify production issues immediately and adjust processes accordingly. Decision-useful product context shows that an industrial checkweigher enhances regulatory compliance by maintaining detailed weight records required by food safety and pharmaceutical authorities. The application suitability of an industrial checkweigher extends across diverse industries including pharmaceuticals, bakeries, snack manufacturers, and beverage producers. Speed and reliability represent critical operational benefits, as an industrial checkweigher maintains consistent performance throughout production shifts without fatigue-related errors. An industrial checkweigher protects brand reputation by ensuring every product meets customer expectations for weight and quality. The return on investment from an industrial checkweigher typically materializes within months through waste reduction alone. Modern industrial checkweigher technology reduces product giveaway by precisely controlling fill weights, directly improving profit per unit. Manufacturers using an industrial checkweigher experience increased customer satisfaction through reliable, consistently weighted products that meet or exceed specifications.

Latest News

All Food Metal Detectors Are Essential Tools: A Focus on Ywan Test

28

Apr

All Food Metal Detectors Are Essential Tools: A Focus on Ywan Test

Ywan Test provides advanced food metal detectors, enhancing safety and efficiency by accurately detecting metal contaminants in food products.
View More
Improving Food Safety with Ywan Test Checkweigher Conveyors

28

Apr

Improving Food Safety with Ywan Test Checkweigher Conveyors

Ywan Test checkweigher conveyors ensure precise weight measurement and compliance, boosting food quality, efficiency, and cost savings.
View More
Reigning Productivity with Ywan Test Logistics Sorting Machinery

28

Apr

Reigning Productivity with Ywan Test Logistics Sorting Machinery

Ywan Test revolutionizes logistics with high-speed, precise sorting machinery, boosting efficiency, reducing costs, and enhancing customer satisfaction.
View More
Best X-Ray Machines for Food Inspection in Factories

01

Nov

Best X-Ray Machines for Food Inspection in Factories

Ywan Test offers top X-ray machines for food inspection, ensuring safety and compliance while enhancing manufacturing efficiency.
View More

industrial checkweigher

Precision Weight Detection Technology

Precision Weight Detection Technology

An industrial checkweigher utilizes advanced load cell technology and sophisticated sensor systems to detect weight variations as small as 0.1 grams, ensuring exceptional accuracy that exceeds manual verification capabilities. This precision is critical for industries where weight specifications are strict legal requirements, such as pharmaceutical and food sectors. An industrial checkweigher's detection technology works continuously at production speeds, processing hundreds of items per minute without compromising measurement accuracy. The real-time feedback system of an industrial checkweigher allows operators to monitor weight trends and adjust filling equipment immediately when drift occurs. This proactive approach prevents batches of out-of-specification products from being produced, saving significant costs and minimizing waste. An industrial checkweigher's ability to maintain precision under varying environmental conditions demonstrates its reliability in demanding manufacturing environments.
Intelligent Rejection and Sorting Systems

Intelligent Rejection and Sorting Systems

An industrial checkweigher automatically identifies and removes non-conforming products through customizable rejection mechanisms that protect your brand reputation and prevent customer complaints. When an industrial checkweigher detects an out-of-spec item, it instantly diverts the product using pneumatic pushers, gates, or conveyor systems based on your configuration preferences. This automated rejection capability of an industrial checkweigher eliminates manual handling and human error in quality control decisions. An industrial checkweigher can be configured to accept variable weight ranges, making it adaptable to different product lines and specifications. The sorting precision of an industrial checkweigher ensures consistent execution throughout production shifts, maintaining quality standards without operator fatigue or attention lapses. Advanced industrial checkweigher models provide categorized rejection options, separating underweight from overweight items for different handling protocols and root cause analysis.
Data Integration and Compliance Documentation

Data Integration and Compliance Documentation

An industrial checkweigher provides comprehensive data logging and reporting features that support regulatory compliance and continuous improvement initiatives across your organization. Modern industrial checkweigher systems connect to manufacturing execution systems, enabling seamless data flow for traceability and audit trail requirements. An industrial checkweigher generates detailed statistical reports showing weight distributions, rejection rates, and production trends that inform process optimization decisions. The compliance capability of an industrial checkweigher helps manufacturers meet stringent requirements from regulatory bodies including FDA, USDA, and international food safety standards. An industrial checkweigher maintains timestamped records of every measurement, creating documentation that protects your company during audits and recalls. Integration features of an industrial checkweigher include Ethernet connectivity, cloud compatibility, and custom reporting interfaces that align with existing quality management systems.

Related Search

Industrial Checkweigher - Precision Weight Control